High-Density Grinding Media Balls for Industrial Applications

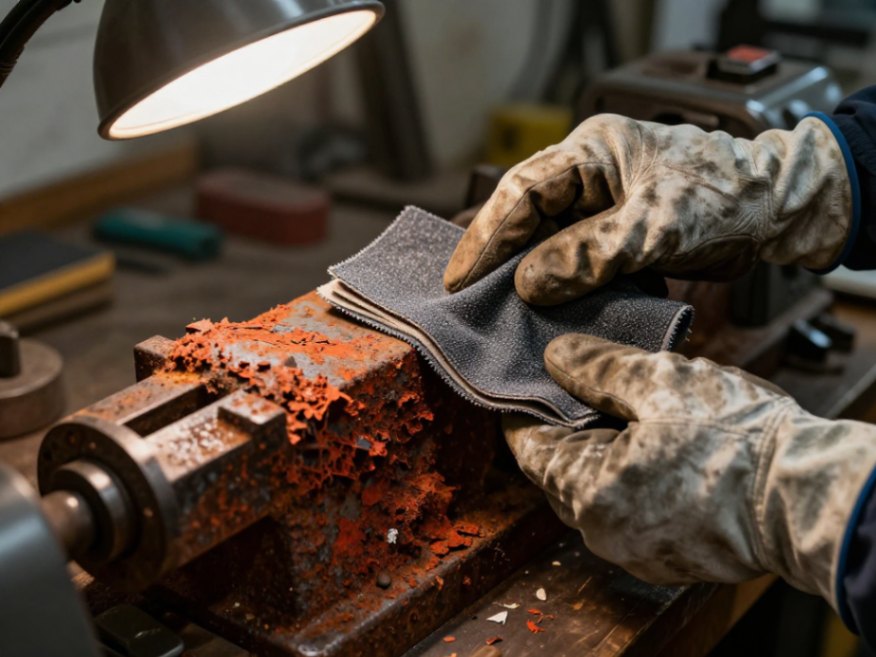
The lathe sat in the corner of the garage for fifteen years. A once-proud machine, its cast iron bed and steel ways wore a thick, scaly blanket of red oxide. The owner, a determined restorer, first attacked it with a wire wheel. It polished more than it removed. Next came 80-grit aluminum oxide on a disc sander. It cut, but clogged almost immediately, gumming up with worn abrasive and metal dust. Frustration mounted until a veteran machinist passed on a single piece of advice: “Stop fighting it. Get yourself some heavy-duty 220 grit silicon carbide cloth and a proper backing pad.” The difference wasn’t subtle. It was revolutionary. This experience, repeated countless times in shops and shipyards, forms the core truth about selecting an abrasive for rust removal. Not all grits are equal. Not all minerals perform the same. We will dissect why heavy-duty 220 grit silicon carbide often represents the optimal point on the curve of cutting speed, surface finish, and durability for serious restoration work.
The Abrasive Landscape: Silicon Carbide vs. The Alternatives
Choosing an abrasive is a technical decision with measurable outcomes. We must compare key properties: mineral hardness, friability (how it fractures), heat resistance, and clogging tendency. Aluminium oxide, the common brown shop abrasive, has a Knoop hardness of about 2100. It’s tough and durable for grinding steel. But its toughness becomes a liability against rust. The abrasive grains round over instead of fracturing to reveal new, sharp edges. They glaze. The binder gets packed with soft oxide debris. Silicon carbide, with a Knoop hardness of 2580, is significantly sharper and harder. Its crystals fracture in a controlled, micro-sharp manner. This self-sharpening action is critical. It maintains an aggressive cutting face throughout the sheet’s life, precisely scraping away rust without loading up as quickly. For rust–a brittle, layered contaminant–silicon carbide’s sharp, friable nature is a targeted advantage. Zirconia alumina is another contender, excelling in high-pressure metal removal, but its cost and over-aggression for surface preparation often place it outside the ideal scope for dedicated rust work.
Why 220 Grit is the Strategic Compromise
Grit selection dictates your workflow. Coarse grits (40-80) remove material fast but leave deep, waveform scratches that must be laboriously sanded out. You trade initial speed for multiple additional steps. Fine grits (400+) polish but lack the cutting aggression to tackle significant oxidation; they burnish more than they remove. The 220 grit specification exists in the sweet spot. It is a medium grit with enough tooth to abrade rust and light pitting effectively, yet it leaves a surface profile–often in the range of 1.5 to 3 mils (38 to 76 microns)–that is exceptionally receptive to primer adhesion. This one-step preparation, moving directly from rust removal to a primer-ready surface, is its greatest economic and practical benefit. It eliminates the two or three intermediate sanding steps required when starting with a coarser abrasive.
Anatomy of a Heavy-Duty Backing
The “heavy-duty” designation is not marketing. It refers to the backing material and the bond. For silicon carbide, this typically means a flexible, tear-resistant cloth backing (often X-weight or Y-weight cotton or polyester-cotton blend) saturated with a waterproof resin. This construction allows the sheet to withstand the lateral forces, heat, and friction generated by orbital sanders, angle grinders with sanding pads, and air files. A “paper” backing, common in fine-finish woodworking sandpapers, would disintegrate in seconds under these conditions. The heavy-duty cloth backing provides the necessary durability for power tool application, conforming slightly to contours without tearing. The bond, the resin that holds the grains, is equally crucial. A strong, heat-resistant phenolic resin locks the sharp silicon carbide crystals in place, maximizing grain utilization before discard.
| Feature | Heavy-Duty 220 Grit SiC | Standard Aluminum Oxide | Wire Wheel/Brush |
|---|---|---|---|
| Primary Action | Controlled cutting/abrasion | Grinding/stock removal | Burnishing/Polishing |
| Surface Profile Created | Ideal for paint adhesion (1.5-3 mils) | Too deep, requires blending | Minimal, often glazes surface |
| Clogging Resistance | High (sharp, friable grains) | Low (grains glaze, load up) | N/A |
| Best Application | Direct rust removal to primer-ready finish | Heavy weld cleanup, shaping | Loose rust, tight corners |
Operational Protocol: The Expert Method
Correct technique extends product life and ensures safety. First, mechanically remove any loose, flaking rust with a scraper or stiff brush. Always wear ANSI-approved safety glasses, a respirator rated for fine particulates (N95 or P100), and heavy-duty gloves. Secure the workpiece. For large, flat areas, use a random orbital sander with a firm foam or rubber backing pad. Set the speed to a moderate 10,000-12,000 orbits per minute (OPM). Let the abrasive do the work; applying excessive pressure only generates heat, glazes the abrasive, and fatigues the user. Move the sander in consistent, overlapping passes. For tighter curves or edges, use an angle grinder fitted with a rubber backing pad designed for sanding discs, operating at 8,000-10,000 RPM. Keep the disc moving to avoid creating grooves. Frequently inspect the abrasive. A loaded sheet cuts poorly. For cloth-backed silicon carbide, a periodic cleaning with a rubber abrasive cleaning stick can restore some efficacy. Discard the sheet when the majority of grains appear dull or the backing shows signs of wear. The goal is to achieve a uniform, dull gray metallic surface with a consistent scratch pattern.
- Safety & Prep: Don PPE (glasses, respirator, gloves). Remove loose scale.
- Tool Setup: Mount 220 grit SiC disc on ROS (10-12k OPM) or angle grinder with sanding pad (8-10k RPM).
- Application: Use moderate, even pressure. Employ overlapping, constant-motion passes.
- Inspection: Check for loaded abrasive. Clean with a rubber stick if needed.
- Completion: Achieve uniform grey substrate. Wipe surface with a tack cloth before priming.
The Final Verdict and Your Next Step
Data and experience converge on a clear conclusion. For the majority of rust removal scenarios where the desired end state is a protected, painted surface, heavy-duty 220 grit silicon carbide on a cloth backing provides the most efficient, single-step path from corrosion to primer-ready substrate. It outperforms aluminum oxide in cut longevity and clog resistance on rust. It creates a superior surface profile compared to coarser grits. Its heavy-duty construction makes it the only choice for power tool use. Your restoration project deserves this level of precision. Do not compromise with hardware store bargain packs. Seek out professional-grade, resin-bonded, heavy-duty 220 grit silicon carbide abrasive cloth. Purchase a ten-pack from a reputable industrial supplier. Test it on a small section. The difference in performance, clarity of cut, and final surface quality will be immediately apparent. This is the tool that separates a lasting restoration from a recurring problem. Make the switch today.
eduloc founded on October 17, 2012, is a high-tech enterprise committed to the research and development, production, processing, sales and technical services of ceramic relative materials such as Heavy. Our products includes but not limited to Boron Carbide Ceramic Products, Boron Nitride Ceramic Products, Silicon Carbide Ceramic Products, Silicon Nitride Ceramic Products, Zirconium Dioxide Ceramic Products, etc. If you are interested, please feel free to contact us.
RELATED POSTS
Iron Gallium Alloy (FeGa ( 82/18 at%))-Sputtering Target
November coke price shock back to the 1 1 2 schedule 40 pipe price of the impact
Why sodium silicate powder has good acid resistance and heat resistance

Plans to increase coal-fired power generation in many European countries have had an impact on solid state spdt relay prices

High Purity Hafnium Diboride Powder HfB2 CAS 12007-23-7, 99%